Second sourcing jerry cans, and what China plus one actually requires
A second factory is not a second source until it is certified as one. The questions that separate a real dual origin from a slogan.
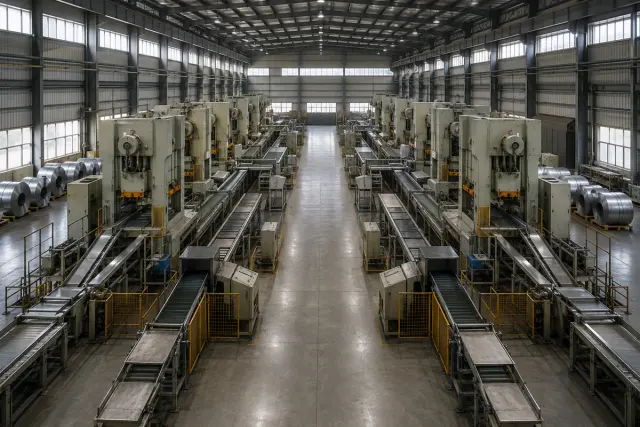
Every packaging supplier now claims a China-plus-one story. Almost none of them mention the part that decides whether it works: a dangerous-goods approval covers a design made at a plant the authority has accepted, and it does not follow your production to a new plant on its own. A second factory is not a second source until it has been certified as one.
Quick answer: What does China plus one mean for packaging buyers?
Holding a second production origin outside China, so a single-country disruption, tariff change or sourcing policy does not stop supply. For dangerous-goods packaging, UN approval is granted per design type, so the second plant must be certified for your design. If it already is, a switch takes one production cycle; if not, re-certification can take months.
What buyers are actually buying
Dual sourcing gets bought for three different reasons, and they need different things from a supplier:
- Continuity is the fear of an empty shelf, and it wants two plants that can each carry the line alone.
- Policy is a sourcing rule that limits single-country exposure, and it wants a documented second origin regardless of whether the first one ever fails.
- Tariff and trade is arithmetic: the same can landed from two origins can attract different duty under different agreements, and the cheaper origin is not always the cheaper landed cost.
Work out which of the three you are solving before you shortlist. A supplier who is excellent for continuity may be useless for a policy that requires an audited origin declaration.
The certification trap
UN approval for a jerrican is granted per design type, and the plant that makes it must work under a quality assurance programme the competent authority accepts. The approval is a certificate naming a design and, through the mark and the audits, the maker. Move the same drawing to a second plant and that plant has to be brought under the approval, with fresh design-type tests where the authority requires them, before it may produce a UN-marked can.
So the promise “we can switch you to our other factory” means one of two very different things. Either the second plant is already approved for your design, in which case the switch is real and can happen in a production cycle. Or it is not, in which case the switch is a re-certification project that can take months, and anything shipped in the meantime is not certified for dangerous goods. Ask which, and ask for both certificate numbers.
Where the authority asks for fresh tests, as Germany’s BAM does by default, re-certification means testing the design type again at the new plant. The tests cover drop testing from the height its packing group demands (with plastics conditioned to −18 °C first), a stack test, a leakproofness test and a hydraulic pressure test. Tooling has to exist and be producing representative parts before any of that starts, because the test is of the design as that plant makes it rather than of the drawing. Our UN packaging codes guide sets out what the marking then records.
Approval does not end once it is granted. Under the packaging construction requirements a manufacturer runs a quality assurance programme with design-type testing inside it, so the plant has to keep demonstrating the design rather than pointing back at a certificate issued years ago. A second plant therefore takes on an ongoing obligation, not just an initial one, and a plant that has been dormant on your design is a different proposition from one that has been running it.
Same drawing is a claim; matched output is the test
Two plants running “the same product” drift unless something stops them. What stops them is one controlled drawing rather than two local ones, and tooling built to the same dimensions rather than each plant’s interpretation. Material is specified by standard and grade rather than by local availability, and first-article parts from both plants are inspected against the same criteria.
The check a buyer can actually run is simple. Ask for a sample from each plant, in the same specification, and measure them:
- Steel gauge.
- External dimensions.
- Closure fit.
- Coating.
If a can from plant A seats in a holder and a can from plant B does not, you do not have a second source. You have two products with one part number, which is worse than one product.
Capacity deserves the same scepticism as certification. A plant that is approved for your design and has never run your volume is a qualified plant, not a proven one. The difference shows up when you need it: in the month you switch, at full rate, with a deadline. Ask what the second plant has shipped of your design, and when. A trial order placed while nothing is wrong is cheap insurance and is the only way to get a real answer.
Dual sourcing is not the only way to buy continuity. Holding buffer stock covers the same risk for many programmes at a known cost in working capital and warehouse space, and it covers it immediately rather than after a qualification. Dual sourcing wins where the exposure is long, where a sourcing policy requires a second origin regardless, or where the two origins carry different duty. Where the exposure is a few weeks of shipping disruption, stock is usually the cheaper answer and nobody sells it to you.
| Ask | A real second source answers | A slogan answers |
|---|---|---|
| Is the second plant approved for my design? | Certificate number, plant named, on request | “We are UN certified” |
| How fast can you switch? | A production cycle, if pre-approved | “Immediately” |
| Whose drawing do both plants build to? | One controlled drawing, held centrally | “Both make the same thing” |
| Can I have a sample from each? | Yes, in the same specification | A sample from whichever is running |
| What changes on my paperwork? | Country of origin, and the duty that follows | Not mentioned |
Origin changes your landed cost, not just your risk
The country a can is made in is declared on the paperwork and determines which trade agreement, if any, applies. Preferential rates under agreements such as AANZFTA turn on rules of origin, not on where the invoice comes from, so switching plants can move your duty rate in either direction. A second source that raises landed cost by more than the risk it removes is a bad trade, and you cannot know which it is until you price both origins to your own destination.
Get an origin declaration from both plants before you need one, and re-run the landed cost per origin rather than assuming the ex-works difference carries through.
How we run it
Production sits in Vietnam and in China, to one specification, with contracts and quality sign-off held in Singapore. That is the arrangement a China-plus-one sourcing policy is written for, and it is why a single-country disruption does not end the conversation.
The section above is a test we should pass too. We hold UN certification for our dangerous-goods designs. Which plant is approved for which design is a question with a real answer, and you should ask for the certificate number and the plant named on it before you rely on a switch. Capacity across the network runs at around 50,000 units a month across four production lines, varying by model. Lead time is approximately one month for a standard run, with samples in 7 to 15 days. We would rather you took a sample from each base and measured them than took our word for the match.
Where to start
Second-sourcing a full range at once is how these projects stall. Start with the line that hurts most if it goes empty.
| Your use case | Recommended can | Why this one |
|---|---|---|
| The line you cannot run out of | 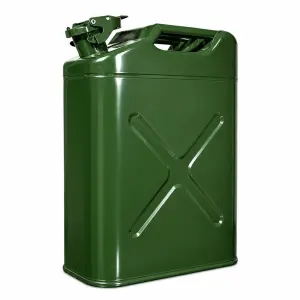 20L NATO Steel Fuel Can |
Highest-volume format, both bases tooled. |
| No coating to match between plants | 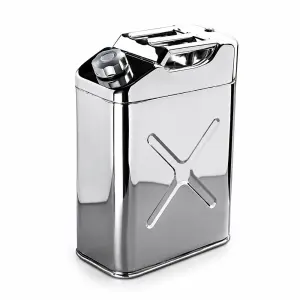 20L Stainless Steel Water Can |
Stainless removes a whole drift risk. |
| Fastest first order | 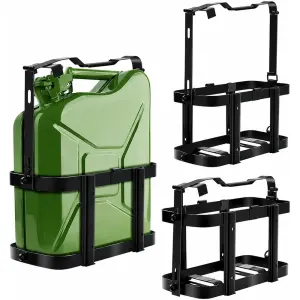 Jerry Can Holders & Mounts |
No dangerous-goods certification in the path. |
| Volume plastic, second origin | 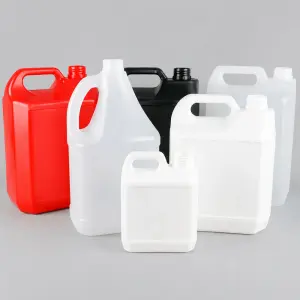 Economy HDPE Jerrycan — non-UN |
Where policy usually bites first. |
Common questions
Does a UN certification transfer if a supplier moves my production to another factory?
Not automatically. UN approval is granted per design type. The competent authority decides what a second plant must show, from its own quality assurance cover and manufacturer marking to fresh design-type tests, before it may produce a UN-marked can for the same drawing. Ask for both certificate numbers before you rely on a switch.
What does China plus one mean for packaging buyers?
Holding a second production origin outside China so a single-country disruption, tariff change or sourcing policy does not stop supply. For dangerous-goods packaging it means more than a second address: the second plant has to be certified for your design, or the switch is a re-certification project rather than a production decision.
How do I check two factories are really building the same product?
Ask for a sample from each plant in the same specification and measure them. Steel gauge, external dimensions, closure fit and coating. If one seats in a standard holder and the other does not, you have two products sharing a part number rather than a second source.
Does changing the country of manufacture affect my import duty?
It can, in either direction. Preferential rates under trade agreements turn on rules of origin, not on where the invoice comes from, so a second origin can raise or lower your duty. Get an origin declaration from both plants and re-run landed cost per origin before you assume the ex-works difference carries through.
How quickly can a supplier switch production between plants?
One production cycle if the second plant is already approved for your design, and months if it is not, because the plant has to be brought under the approval first, with re-testing where the authority requires it. Any supplier answering "immediately" without naming a certificate has not understood the question.
References
The standards and regulations this page relies on, at their issuing body. Where a market rule is named here, check the current revision before you specify against it.
First published
Last reviewed by David Guru, Co-Founder & Business Development Director. How we review our guides Fortitude21 makes and sells liquid containers; our guides carry no affiliate links.
Talk to us about your sourcing programme
Tell us your market, the products and your volumes. We come back with the production base for each line, a specification sheet and a quotation.